Industries
Global Manufacturing Leaders Choose CFI to Support More Profitable Innovation
At CFI, we drive more profitable innovation for the global industrial leaders we serve with sustainable consistency in quality products, source stability, logistics, and service. For more than 30 years we have helped manufacturers improve formulas, end products, and processes in markets where product consistency and delivery require precision. We also extend an invaluable commitment to collaboration in testing new applications in both our core industries and in new markets like asphalt paving and construction products.
Global industries we serve:
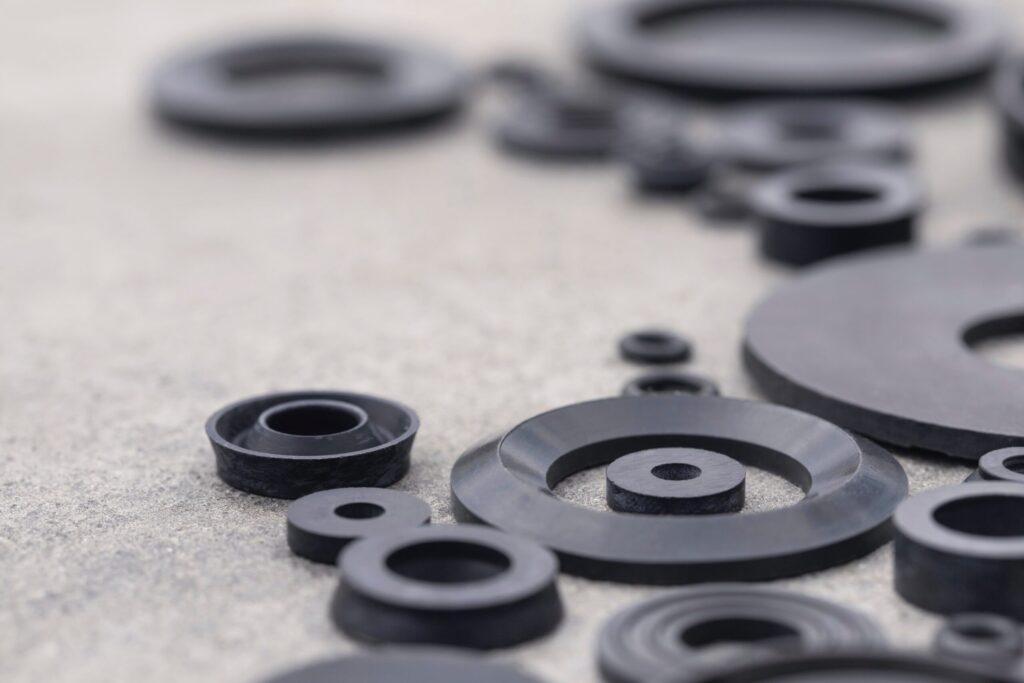
Sample Applications
- Automotive Passenger and Light Truck Tires
- Lawn and Garden, Trailer/Hauler, ATV/UTV, Agriculture, Construction, and Industrial Tires
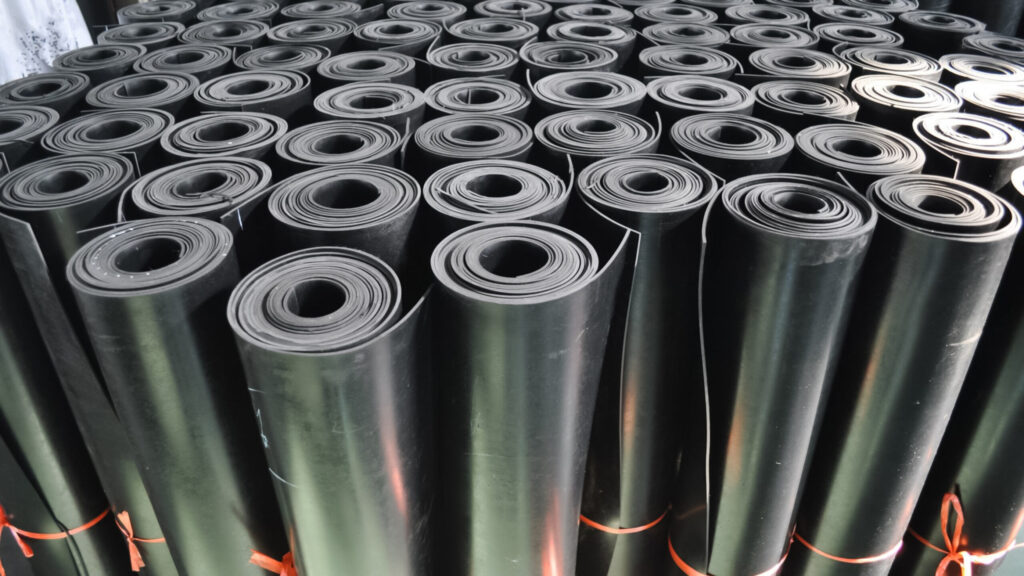
- Office and Industrial Mats
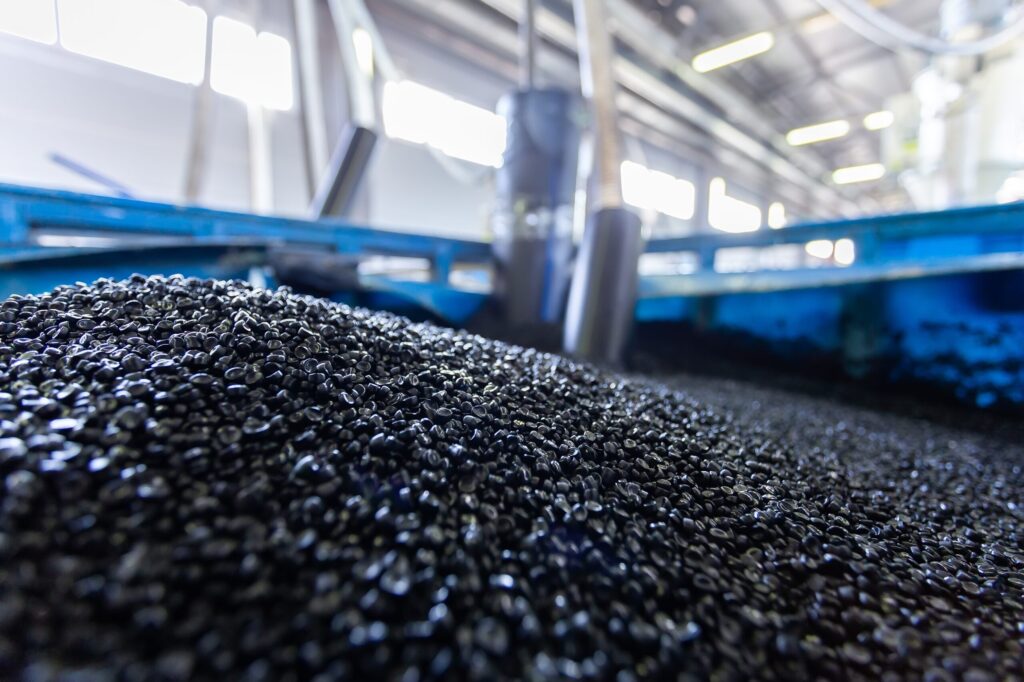
- Black Plastic Masterbatch
- Custom Compounders
- Rubber Boat Trailer Rollers
- Mastic Solvent-Based Material
- Window Spacers
- Epoxy and Roof Coatings
- Automotive Door Seals, Hoses and Belts, Mud Flaps, and Engine Mounts
- Cured and Uncured Rubber Seals
- Railroad Pads
- Black Polyurethane Adhesive
- Fluoroelastomers
- Plasticizers
- Conveyor Belts
- Unloading Dock Rubber Bumpers
- Rubber Casters
Austin Black 325 is Produced Via a Low CO2 Emissions Process.
We Partner with Manufacturing Leaders in Over 30 Countries
We make global collaboration easy with translation services, strategic distributor relationships worldwide, and highly controlled operations to ensure on-time delivery.
Frequently Asked Questions
Which industries use carbon black the most?
Carbon black is primarily used in the rubber, plastics, coatings, and construction industries. Its ability to reinforce, color, and improve conductivity makes it versatile across sectors.
How does carbon black enhance rubber performance?
In rubber manufacturing, carbon black increases tensile strength, abrasion resistance, and longevity, making it essential for high-stress products like tires and gaskets. Learn more on our Rubber Applications page.
Are your carbon black products customizable for specific industries?
Yes, CFI offers tailored solutions based on your industry’s specifications. Whether it’s particle size, tint strength, or dispersion, we work with you to deliver optimal performance.
Is carbon black safe for use in consumer products?
Our carbon black products meet industry safety standards and are used in a variety of consumer-safe applications including packaging, household plastics, and inks.
How do I choose the right carbon black for my industry?
The right carbon black depends on the desired properties—reinforcement, coloration, or UV stability. Explore our Carbon Black Products to compare options.