Article Summary
A moisture resistant filler for rubber is a hydrophobic filler that adds volume and property control to a compound without raising water uptake. Buyers also use the same phrase for cartridge pastes and rubber repair putty that fill a crack in a finished rubber surface.
The table gives the short version. The sections after it give the chemistry, the test data, and the cost math.
| Topic | Short answer |
|---|---|
| What “filler” means in search | Two different products: a paste that cures in place inside a void, or a dry powder mixed into a compound before cure |
| Who buys it | Compounders, product engineers, and maintenance buyers in seals, gaskets, hose, roofing, and buried goods |
| Property that decides it | Surface character of the particle (hydrophobic or hydrophilic) plus moisture content of the powder as shipped |
| Failures it prevents | Water swell, hardness loss, blisters under coatings, bond loss at inserts, rust on embedded metal |
| Decision drivers | Water pickup, volume swell, specific gravity, cure compatibility, cost per volume |
| How to prove it | Immersion data on a control compound next to a trial compound, then one line trial |
What a Moisture Resistant Filler for Rubber Actually Does
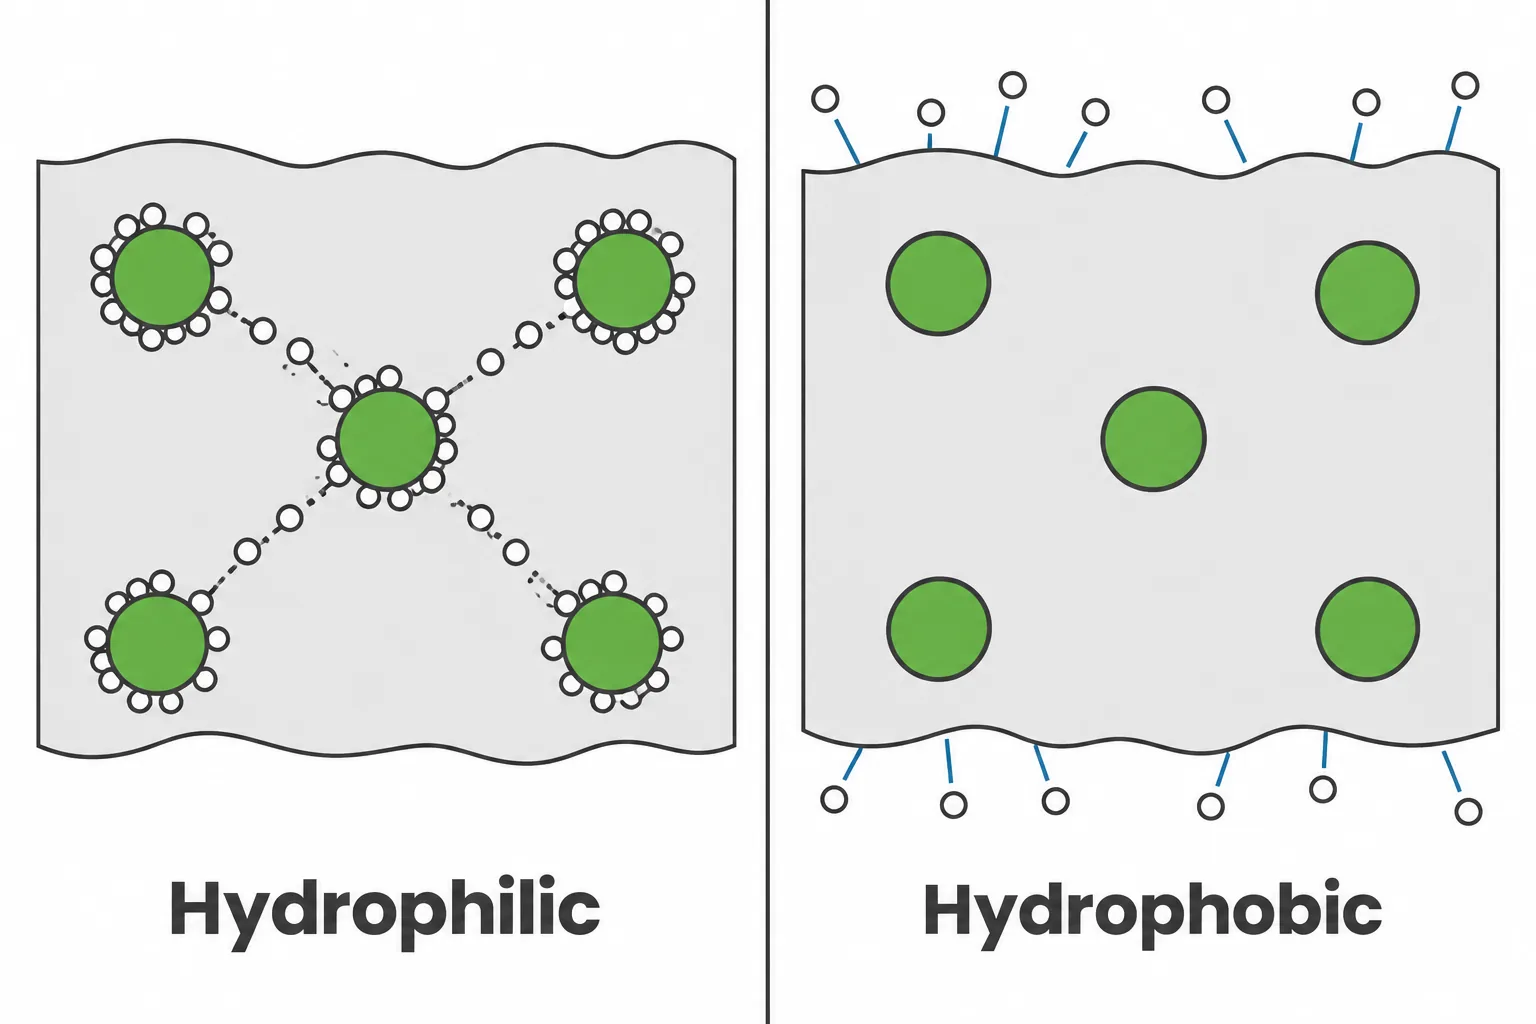
A filler holds down three jobs at once. It occupies volume, which drives compound cost and stiffness. It reinforces or semi-reinforces, which sets tensile strength, tear resistance, and abrasion life. And it decides how the compound behaves around water, because the particle surface is where water gets either rejected or held.
Surface character is the part most buyers skip. A hydrophilic particle carries a polar surface that attracts water molecules. Load millions of those particles into a rubber matrix, and the result is a population of tiny wet sites plus a route for water to travel between them.
A hydrophobic, water repellent particle pushes water away at the surface, so the polymer stays the main moisture barrier and the filler does not undercut it. That single difference explains most of the gap between a moisture resistant filler for rubber and a cheap bulking powder.
The bill for a poor pick arrives after the part ships. Common symptoms: high water uptake (weight gain after immersion), a drop in durometer, blisters below a coating, bond failure where rubber meets a metal insert, and corrosion on that insert while the rubber still looks sound.
Dimensional change follows, and a seal that grew two or three percent no longer sits correctly in its groove. Filler choice also drives color, cure rate, and mill behavior, so a review of what a filler contributes to a rubber compound belongs at the front of any substitution project, not the back.
Repair Paste vs Mix-In Filler: Two Different Purchases
Both products answer a water problem, but they sit at opposite ends of a part’s life. One repairs a part that already exists. The other builds the property into every part you mold next year. The table sorts them out.
| Point of comparison | Repair sealant or paste | Dry mix-in filler |
|---|---|---|
| Form | Cartridge, pail, or brushable liquid | Finely divided powder |
| Where it goes | Into a crack, gap, or void on a finished part | Into the internal mixer or on the mill with polymer, curatives, and other rubber additives |
| Cure | In place, by humidity, oxygen, or a second component | With the compound, during vulcanization |
| Who buys it | Maintenance, facilities, field service | Compound development, purchasing, R&D |
| Right call when | One asset needs to stop leaking this week | Production parts must resist water by design |
| Main limit | Adhesion depends on surface prep and the substrate elastomer | Requires formula work and a trial before release |
A paste patches one part. A powder fixes the next ten thousand.
Bond chemistry sits close to this subject, and the same logic that governs adhesive additives applies here: the interface, not the bulk, decides whether water gets a foothold.
How Water Gets Into a Rubber Part
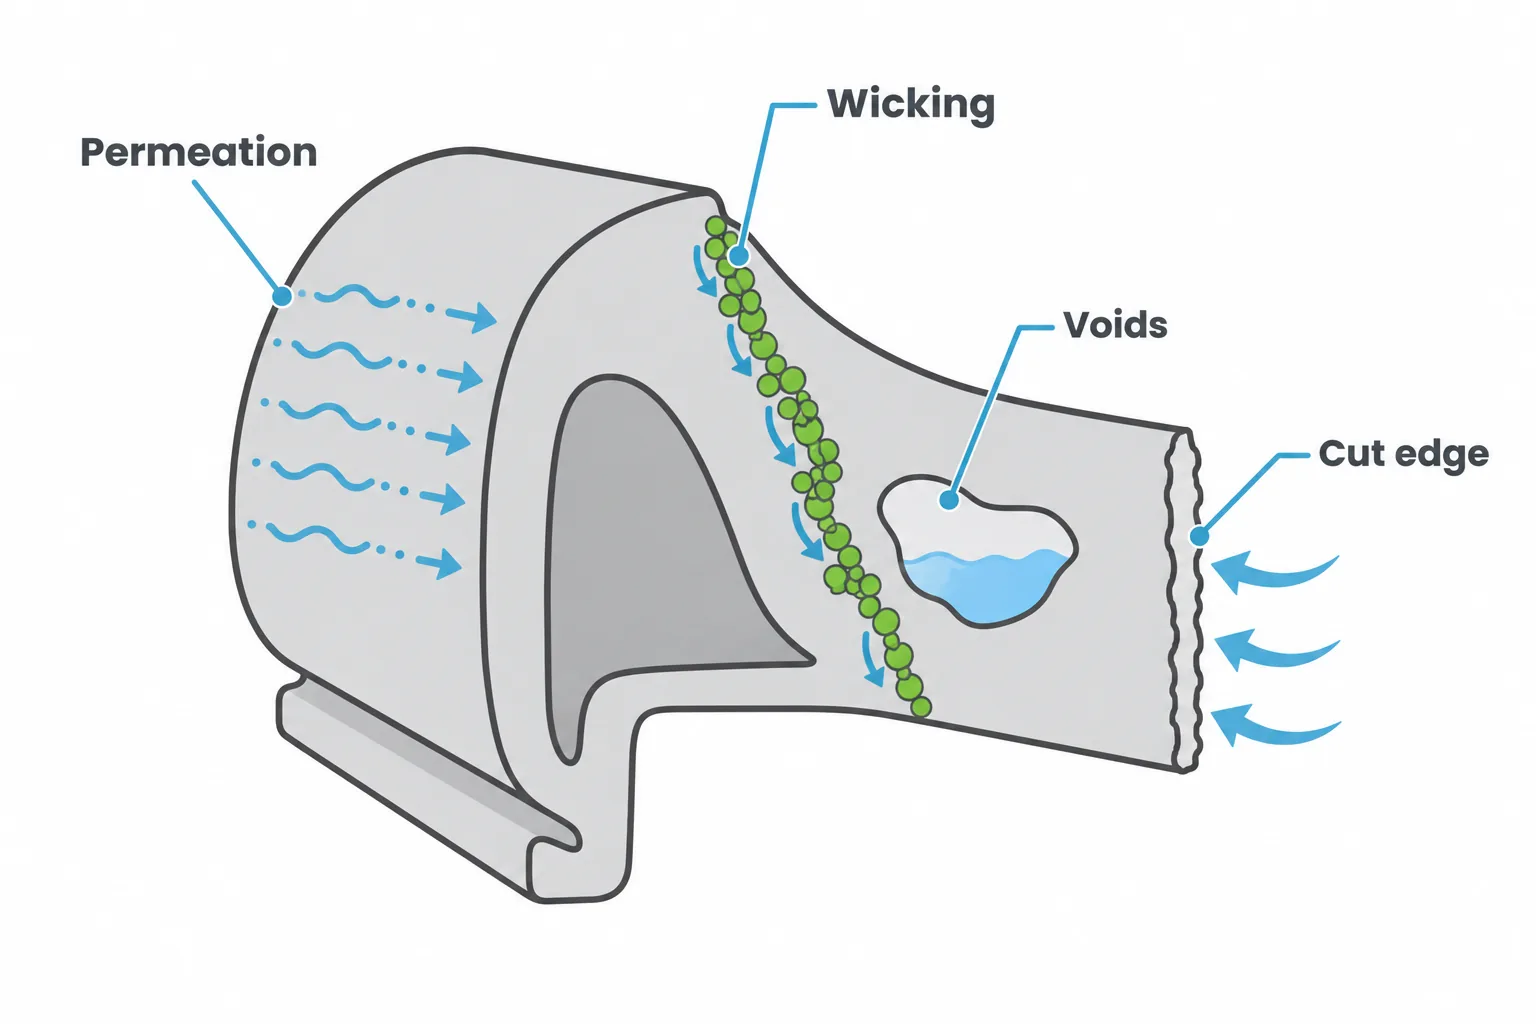
Water does not need a hole. It has four routes into a molded part, and only one of them looks like damage.
| Route | How it works | What limits it |
|---|---|---|
| Permeation | Water vapor dissolves in the polymer and diffuses through it | Polymer type and part thickness |
| Capillary wicking | Water travels along the surfaces of polar filler particles that sit close together | Filler surface character and loading level |
| Voids and porosity | Poorly dispersed agglomerates leave gaps that hold liquid water | Mix quality and dispersion |
| Cut or unsealed edges | Trimmed edges and flash lines expose raw compound and fabric plies | Design, trim practice, edge sealing |
Two secondary effects follow. Absorbed water swells the compound, which changes dimensions and drops hardness. Water also extracts soluble ingredients, so a compound built with hygroscopic plasticizers or salt-bearing residues loses part of its recipe after long immersion.
Polymer selection sets the baseline before any filler enters the picture. Butyl vulcanizates show very high aging resistance and limited permeability to gases and liquids, which is why butyl turns up in liners and sealing tapes. EPDM handles weather and water service well.
Nitrile earns its place on oil resistance, not water resistance, and its polar backbone is a factor in wet duty. Once the polymer is fixed, filler choice moves water uptake up or down from that baseline, and the role of carbon black in rubber compounds is a useful reference point for how large that shift can be.
Filler Options Ranked by Moisture Behavior
Fillers split cleanly into two camps: organic particles with nonpolar surfaces, and mineral particles with polar ones. The table ranks the common choices by wet-duty behavior, with reinforcement and density beside them, because no plant selects on water alone.
| Filler | Surface character | Moisture pickup tendency | Reinforcement | Typical specific gravity | Common use |
|---|---|---|---|---|---|
| Furnace carbon black | Hydrophobic | Low | High | About 1.8 | Tires, hose, seals, technical goods |
| Precipitated silica | Hydrophilic | High | High, with a coupling agent | About 2.0 | Tread, footwear, white and light compounds |
| Kaolin clay | Hydrophilic | Moderate to high | Semi-reinforcing | About 2.6 | General purpose, cost reduction |
| Ground calcium carbonate | Hydrophilic | Moderate to high | Non-reinforcing | About 2.7 | Volume filler, low-cost goods |
| Talc | Hydrophilic, platy | Moderate | Non-reinforcing | About 2.8 | Barrier and stiffness, dusting |
| Austin Black 325 (coal-based organic filler) | Hydrophobic | Low | Semi-reinforcing | 1.3 | Seals, gaskets, roofing, molded goods, wire and cable |
Silica carries a process penalty. Its polar surface holds atmospheric moisture, so silica compounds normally require a silane coupling agent, longer mix cycles, and controlled drying before use. Those steps work, and plenty of wet-service parts run silica successfully, yet the process carries more variables than a hydrophobic filler does.
Clay and calcium carbonate cost less per pound than almost anything else on the list, and their mineral surfaces are the reason they belong in dry service rather than in immersed or buried parts.
Austin Black 325 sits in a different category from the minerals. It is made from low-volatile bituminous coal, so the particle is organic and its surface behaves like carbon rather than like a silicate.
Anyone who compares options across grades and structures will find a breakdown of filler grades and their property trade-offs helpful when a formula needs both water resistance and a target modulus.
Austin Black 325 in Wet-Service Compounds
Austin Black 325 is CFI Carbon Products’ flagship filler: a finely divided powder produced from high-quality, low-volatile bituminous coal. Two properties drive its use in wet and buried parts. The surface is hydrophobic, so it does not create wicking paths through the matrix. And its density is low for a filler.
CFI’s published technical data and resource library lists a specific gravity of 1.3 for Austin Black 325, against roughly 1.8 for furnace carbon black, so a compound carries fewer pounds at equal filler volume.
Compounds are designed by volume and purchased by weight. A lighter filler fills the same space with fewer pounds, so cost per cubic inch of finished compound falls even when cost per pound looks similar. Processability improves as well, and the finished part weighs less, which shows up in freight and in handling on the line.
Typical fits: seals and gaskets, roofing membrane, molded industrial goods, hose covers, and anything destined for outdoor or buried service. The filler also appears in tire and industrial applications where cost per volume and specific gravity carry weight in the formula, and the comparison of options for tire and industrial rubber fillers covers that ground.
CFI runs formula testing and lab sampling, offers toll grinding, and handles custom packaging, so a compounder can trial a substitution against a control recipe before a production batch is committed.
Compound Design Rules for Wet and Buried Service
A water resistant rubber compound is not built from a single ingredient. Six levers move it, and a plant that pulls only one usually gets a disappointing result. Each lever below has a known direction of effect.
Related readingLow Density Filler for Rubber: A Formulator’s GuideRead the guide →| Lever | Effect on water uptake | Practical note |
|---|---|---|
| Polymer selection | Sets the floor for permeation | Butyl, EPDM, and CR suit wet duty better than polymers with polar backbones |
| Filler type | Raises or lowers wicking and surface adsorption | Hydrophobic organic particles beat polar minerals in immersion |
| Filler loading | Higher loading of a polar filler multiplies the problem | Loading targets should be set by volume, not by weight |
| Plasticizer choice | Hygroscopic or water-extractable plasticizers pull water in | Favor low-polarity process oils compatible with the polymer |
| Cure system | Residues and salts can be water-soluble | Keep soluble accelerator residues and metal salts low |
| Dispersion quality | Agglomerates leave voids that hold liquid water | Mix time and sequence matter as much as the filler spec |
Water-soluble content is the quiet failure mode. A compound can carry an excellent filler and still gain weight in a 70-degree C immersion test because an ingredient leaches and leaves osmotic sites behind. That is why immersion data on the full recipe beats data on any single component.
Roofing shows the stacked-load case clearly. A membrane takes standing water, thermal cycling, and full sun on the same surface, so the formula has to satisfy weathering, UV protection, and water resistance at once, alongside the polymer processing additives and specialty additives that keep a wide sheet running at line speed.
The material choices behind rubber roofing membrane follow the same reasoning as those behind buried seals, with UV load added on top.
Sealants and Pastes That Bond to Rubber
If the job is a crack in an existing rubber surface rather than a new compound, the purchase is a sealant or a surface filler for rubber. Five chemistries cover nearly every case, and they differ mainly in movement capability and in how they cure.
| Chemistry | Cure mechanism | Gap and movement | Behavior on rubber | Watch for |
|---|---|---|---|---|
| RTV silicone (neutral cure) | Ambient humidity | Wide gaps, high movement, stays flexible | Good on silicone and EPDM with prep | Acid-cure types can attack some substrates and metals |
| Moisture-cure polyurethane | Ambient humidity | Wide gaps, high movement | Strong bonds, paintable | Slower cure in dry air, skins from the outside in |
| Butyl | Solvent release or pre-formed tape | Low movement, good water barrier | Tacky, sticks well to clean surfaces | Creeps under load, not structural |
| MS polymer (silane-modified) | Ambient humidity | Wide gaps, high movement | Broad adhesion, low odor | Higher cost than silicone |
| Rubber-toughened cyanoacrylate | Surface moisture | Tight joints only, minimal gap | Fast grip on small tears | Brittle in thick sections, no gap tolerance |
Polyurethane earns its reputation in wet joints because of how it sets. Most polyurethane sealants are one-part systems in which isocyanate-terminated prepolymers react with ambient humidity to build a crosslinked elastomer from the surface inward. The cured film stays elastic, so a joint that moves does not tear the seal.
Surface prep decides the outcome more often than chemistry does. Clean the area, abrade it lightly to break the surface glaze, degrease with a solvent the elastomer tolerates, and let it dry fully.
Then test on a scrap piece of the same rubber before you commit to the repair, because mold release, plasticizer bloom, and antiozonant migration all interfere with adhesion.
Several automotive-grade RTV silicones and urethane sealants are rated for elastomer contact, and the manufacturer’s technical data sheet is the authority on substrate compatibility and service temperature.
Formulated sealants and paints lean on the same toolkit of coating additives for color, rheology, and weathering that a rubber compound uses for its own targets.
Tests and Data to Request From a Filler Supplier
A supplier claim is a starting point. Data on your own recipe is the decision. Request the items below, in writing, before any trial.
| Data item | Method or spec | What it tells a buyer |
|---|---|---|
| Water immersion results | ASTM D471, volume, mass, and hardness change | Direct measure of swell and property loss in water |
| Heat aging | Tensile and elongation retained after oven aging | Whether the compound survives wet plus hot duty |
| Moisture content as shipped | Supplier spec, percent by weight | Risk of porosity and cure interference during mixing |
| Particle size and sieve residue | Sieve analysis, percent retained | Dispersion behavior and surface finish |
| Specific gravity | Supplier data sheet | Cost per volume and finished part weight |
| Lot-to-lot records | Certificate of analysis history | Consistency across production batches |
The immersion number is the one to insist on. The ASTM D471 liquid-immersion test method covers the procedures for evaluating how vulcanized rubber and rubber-like compositions withstand the effect of liquids, which makes it the common language between a compounder and a filler supplier.
Run it on a control compound and a trial compound from the same mix cycle, same cure, same coupon geometry.
Four questions belong in the same email: what is the moisture content spec, how should the powder be stored and handled, how tight is lot-to-lot consistency, and what is normal lead time. Reputable plastic additives manufacturers and industrial additives suppliers answer all four without hesitation.
Ask for a lab sample as well, since a small bench batch costs far less than a failed line trial. CFI supports this path directly through formula testing and lab sampling, the same service pattern used when a plant evaluates polyurethane additives or other polymer additives against a new spec.
Cost and Sustainability Math Behind the Filler Swap
Purchasing works in dollars per pound. Compound design works in volume. A filler with low specific gravity fills the same space with fewer pounds, and that arithmetic is where a swap pays for itself. The table uses published density figures and one liter of filler volume as the reference.
| Basis | Filler at 1.8 specific gravity | Filler at 1.3 specific gravity |
|---|---|---|
| Mass to fill 1,000 cubic centimeters | 1,800 grams (about 3.97 lb) | 1,300 grams (about 2.87 lb) |
| Relative pounds purchased at equal volume | 100 | About 72 |
| Effect on finished part weight | Baseline | Lower at the same volume loading |
| Effect on freight per part shipped | Baseline | Lower, on weight-rated shipments |
Roughly 28 percent fewer pounds for the same filler volume changes the cost picture even when price per pound is close. Lighter parts also ship cheaper and handle more easily on the line.
The sustainability side follows from where and how the material is made. CFI Carbon Products, founded in 1987 and privately held, produces its filler in West Virginia and Virginia at sites near the raw-material source, with low CO2 emissions in the production process and control over its own logistics.
Distribution runs through 11 partners and reaches more than 30 countries, which keeps lead times workable for plants outside the United States.
For teams that weigh carbon black alternatives or build an eco friendly rubber program with real numbers behind it, the comparison of eco-friendly rubber alternatives lays out where an organic filler fits and where it does not.
Frequently asked questions
What sealant will stick to rubber?
What is a good water-resistant glue for rubber?
Can automotive RTV-type sealants be used on rubber?
What is a good flexible sealant for rubber?
Does a moisture resistant filler for rubber change compound cost?
Is coal-derived filler the same as carbon black?
Talk to CFI About a Sample
The fastest way to settle a filler question is a bench batch. Request a lab sample of Austin Black 325 and run it beside your current control compound, with immersion and hardness data on both.
CFI’s formula testing and lab services cover that work, and the rubber industry page lists the application areas where the filler already runs in production.